Round Hole Aluminum Perforated Sheet Engineering for Cladding Facades
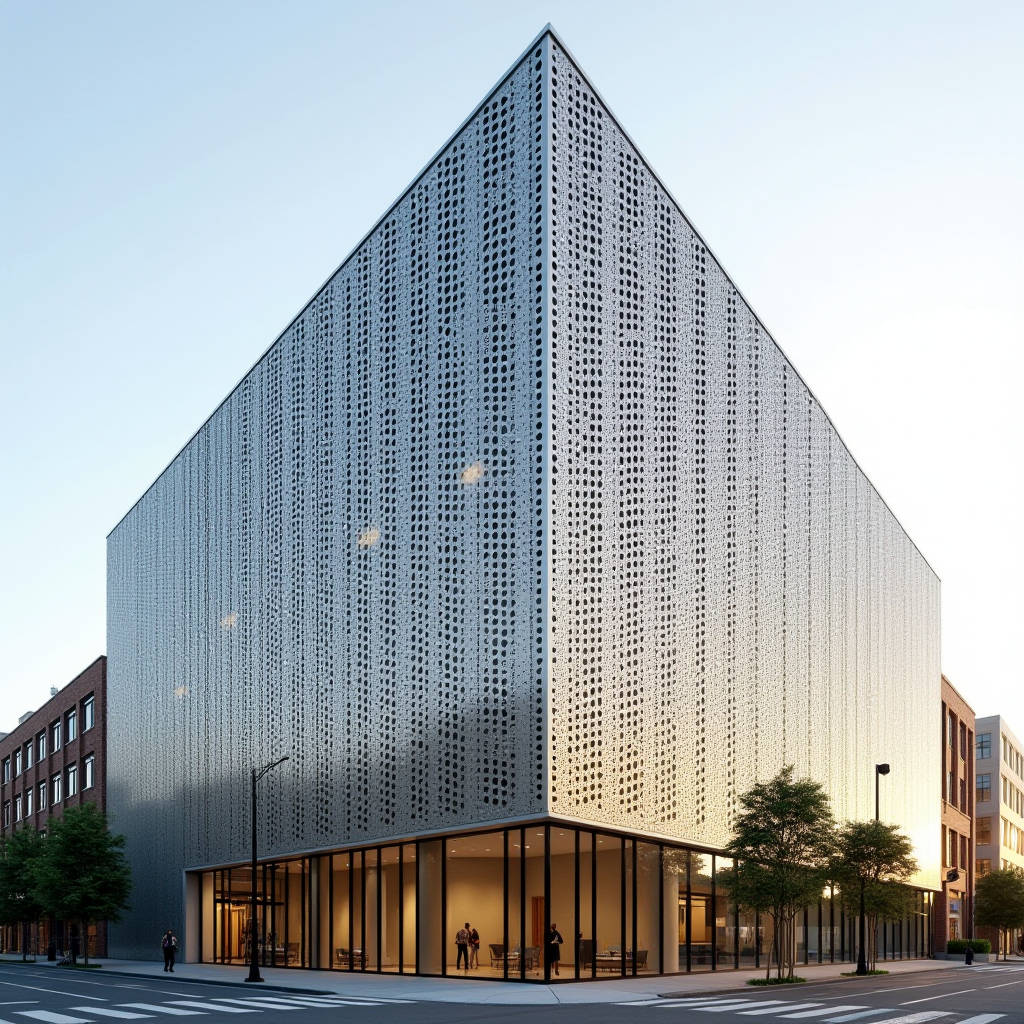
A round hole aluminum perforated sheet is rarely specified for its own sake. It is chosen because a facade, a soffit, a sunshade, or a mechanical screen must solve two problems at once: control light, air, and visibility while carrying structural and weather loads as a solid metal skin. The round perforation is the most predictable opening geometry available to a fabricator, which is why it dominates architectural screening. But predictability on the drawing board does not remove the engineering questions that follow: what happens to the panel at the specified open area, how does the coating perform at every punched edge, and how does the installed system behave under wind load. This article works through those questions from the perspective of a cladding fabricator and a facade engineer, using solid aluminum sheet in 2.0, 2.5, and 3.0 mm thicknesses.
Why the Round Hole Survives Every Specification Debate
Architects often begin with decorative patterns, then return to the round hole once cost, tooling, and lead time enter the conversation. A round hole aluminum perforated sheet punches cleanly with a standard round punch and die, leaves a uniform edge, and produces a predictable open-area percentage from a simple formula. Square, slotted, and hexagonal openings all require dedicated tooling and generate stress concentrations at their corners that round geometry avoids. For a procurement manager, the round hole also means that multiple fabricators can quote the same drawing without one of them holding a proprietary punch profile. That competition is exactly what keeps a bid honest.
The round hole also behaves better under repeated loading. A punched edge is a discontinuity in the metal, and every discontinuity is a place where fatigue can begin. A circle distributes stress evenly around its circumference, while a square or slot concentrates it at the corners. For exterior screens exposed to years of wind cycling, that difference is not cosmetic. It is the reason facade engineers accept higher open-area percentages in round-hole panels than they would in a slotted panel of the same gauge.
Open Area, Gauge, and the Stiffness Trade-Off
The single most important number on a perforation drawing is the open area percentage, and it drives everything downstream. Open area is calculated from the hole diameter and the staggered or straight pitch. A 6 mm hole on a 10 mm staggered pitch yields roughly 32% open area, while the same hole on a 16 mm pitch drops to about 13%. The facade designer wants high open area for ventilation and transparency; the structural engineer wants low open area to preserve panel stiffness; the fabricator wants a pattern that leaves enough solid metal between holes to prevent the sheet from tearing during punching.
There is no free lunch in this negotiation. Every percentage point of open area removes metal that was carrying load, and the loss is not linear. Perforating a solid sheet reduces its effective stiffness more sharply than the simple area loss suggests, because the remaining ligaments between holes begin to act like a series of small beams. A 3.0 mm solid aluminum panel perforated to 40% open area can lose more than half of its bending stiffness compared with the unperforated sheet. This is why thicker gauges are common on high-open-area screens: the fabricator starts with more metal so that what remains after punching is still stiff enough to span the intended support spacing.
Futeng® has supplied round hole aluminum perforated sheet projects where the same visual pattern was achieved at two different gauges on the same building, with 3.0 mm sheet used on the windward elevation and 2.5 mm on sheltered walls, purely to hold deflection within the same limit. The pattern looked identical from the street, but the engineering behind it was not.
Coating Performance at the Punched Edge
A solid aluminum cladding panel is typically coated before or after perforation, and this decision matters more than many specifiers realize. When a pre-coated sheet is punched, every hole exposes a raw aluminum edge. That edge is the most corrosion-vulnerable surface on the entire panel, and it is also the surface least likely to receive a full protective film. When a sheet is punched first and then coated, the coating can wrap into the hole, but liquid coatings pull thin at sharp edges and powder coatings can bridge or pinhole at the rim.
The industry answer is a combination of process discipline and realistic expectations. For a PVDF-coated round hole aluminum perforated sheet, the punched edge will always carry less coating than the flat face, and the specification should acknowledge that. AAMA 2605, the standard for high-performance organic coatings on aluminum extrusions and panels, sets the bar for the face of the panel; the hole interior is governed by practical application limits. Fabricators who care about longevity will deburr every hole, apply a chromate or chrome-free pretreatment that reaches into the opening, and specify a coating system with proven edge coverage.
The corrosion risk is also a function of environment. A marine or industrial atmosphere attacks a bare edge far faster than a dry inland site. For coastal work, many engineers specify a heavier coating, a marine-grade alloy such as 5052 or 5754, or both. The alloy choice is often overlooked in perforated work, but 5xxx-series aluminum carries significantly better salt-spray resistance than the 3xxx alloys sometimes used for flat sheet.
Wind Load and the Perforated Reality
Perforated panels are frequently treated as if they were solid when wind load is calculated, and that assumption can be dangerous in both directions. A screen with low open area does block wind, but it does not block it the way a solid panel does. Air passes through the holes, and the pressure difference across the panel depends on open area, hole size, and the depth of the cavity behind it. A highly perforated screen may see dramatically reduced net pressure, which is good for the panel but bad for whatever sits behind it, since the wind now reaches the inner layer.
The conservative and common approach is to design the perforated panel for a reduced pressure coefficient based on open area, while still detailing the backup wall or inner glazing for the full load. Standards such as ASCE 7 provide the framework for wind pressure, but the perforation reduction factors come from wind-tunnel testing or published research rather than a single code table. A facade engineer should not guess.
Deflection, not strength, usually governs a perforated panel. Because stiffness falls faster than strength as open area rises, a panel may be perfectly safe in terms of ultimate load yet visibly oil-can under service wind. The remedy is a thicker gauge, a smaller unsupported span, or a stiffer support frame behind the perforated sheet. All three cost money, which is why open-area decisions should be locked before the support system is priced.
Gauge, Hole, and Pitch: A Working Reference Table
The table below summarizes a practical set of round hole aluminum perforated sheet configurations for exterior cladding and screening, with the open area, the recommended minimum gauge for a 600 mm span, and the primary design driver for each. These are engineering starting points, not substitutes for project-specific calculation.
| Hole Diameter | Pitch (Staggered) | Open Area | Min. Gauge (600 mm Span) | Primary Design Driver |
|---|---|---|---|---|
| 4 mm | 8 mm | ~23% | 2.0 mm | Visual density, moderate screening |
| 6 mm | 10 mm | ~32% | 2.5 mm | Ventilation and partial transparency |
| 8 mm | 12 mm | ~40% | 3.0 mm | High airflow, solar shading |
| 10 mm | 14 mm | ~46% | 3.0 mm | Maximum transparency, low wind |
The relationship in the table is consistent: as open area climbs, the required gauge climbs with it to hold deflection. A specifier who asks for 46% open area in 2.0 mm sheet on a 600 mm span is asking a panel to do something the metal physics will not support.
Alloy, Temper, and Flatness After Punching
Punching introduces internal stress into the sheet, and that stress shows up as distortion. A large perforated panel that looked flat as a solid blank can come off the press with a visible wave, especially near the edges where the hole pattern stops. The fabricator controls this through alloy and temper selection, punch sequencing, and post-punch leveling.
For flat architectural panels, 3003-H14 and 5052-H32 are the two workhorse alloys. The 3003 alloy punches easily and levels well, which makes it economical for interior and low-exposure screens. The 5052 alloy costs more but brings higher strength and better corrosion resistance, and it resists distortion during punching better at larger panel sizes. When a project demands a large-format round hole aluminum perforated sheet with tight flatness tolerance, 5052-H32 is usually the safer call despite the price premium.
Flatness after perforation is also a function of the margin, the unperforated border left around the panel edge. A generous margin stiffens the panel and gives the fabricator a place to attach stiffeners or folded returns. Cutting the margin to save material is a false economy, because the resulting panel will be harder to keep flat and harder to mount.
Finishing Sequence: Punch First or Coat First
The sequence question divides fabricators, and both answers are defensible. Punching before coating lets the finish reach into each hole, which is better for corrosion protection, but it makes the coating line harder to run because the perforated sheet is flimsier and the coating can bridge across small holes. Coating before punching gives a perfect face and a fast press cycle, but it leaves raw edges in every hole.
The best answer depends on hole size and environment. For large holes above 8 mm, punch-first coating can genuinely wrap the edge and is worth the handling difficulty. For small, dense holes below 5 mm, coating-first is often the only practical route, and the exposed edges are small enough that a good pretreatment and a quality PVDF system will carry the panel through a normal service life in a non-aggressive environment. In marine conditions, a punch-first process with a AAMA 2605-compliant coating is the defensible specification, and the cost should be accepted rather than negotiated away.
Attachment, Stiffening, and the Hidden Frame
A perforated panel is weaker than a solid panel of the same gauge, so the way it is attached matters more. The two common routes are a folded-tray panel with returns on all four edges, or a flat sheet mechanically fastened to a separate subframe. The folded tray is stiffer and cleaner, but the returns add cost and complicate the perforation pattern at the corners. The flat sheet on a subframe is cheaper per square meter but depends entirely on the subframe for flatness.
For large perforated screens, the subframe approach dominates because it allows the perforation to run edge to edge with no folded borders, which is usually what the architect wants visually. The subframe members sit behind the sheet and are hidden by the pattern, and the sheet is fastened with screws or rivets through the solid ligaments between holes. Fastener placement must respect the hole layout so that a fastener never lands on a hole, which is another reason the hole pattern should be fixed before the support frame is detailed.
Stiffening ribs are often welded or bonded to the back of a large perforated panel to control oil-canning. Welding a perforated sheet is more difficult than welding a solid sheet because the holes interrupt the weld path and the heat distorts the thin ligaments. Fabricators with real perforated-panel experience will choose bonded or mechanically attached stiffeners over welding where the pattern is dense, and reserve welding for low-open-area panels with solid margins.
Cost Drivers That Show Up After the Bid
Procurement teams often price a round hole aluminum perforated sheet by the square meter of material and miss the cost drivers that appear only in fabrication. Open area is the biggest one: a 40% open area panel punches nearly twice as many holes per square meter as a 20% panel, which means roughly double the press time and double the tool wear. Hole diameter matters too, because small holes require more strokes and finer tooling.
The material yield is another hidden cost. Perforating does not remove scrap in the same way as cutting a blank, but the margin, the pattern layout, and the panel size all affect how much of each sheet becomes usable panel. A poorly nested pattern can push material waste well above the 10% to 15% a fabricator budgets on solid cladding. Finally, finishing cost rises when the panel must be coated after punching, because the perforated sheet is harder to handle on the line and may need masking or slower conveyor speeds.
The honest way to budget is to price the perforation as a separate line item per hole count or per open-area band, not as a flat percentage on top of the solid-sheet price. A fabricator who quotes 40% open area at the same rate as 20% is either subsidizing the job or has not built one before.
Specifying the Round Hole Without Regret
A clear specification prevents most of the disputes that arise on perforated projects. The drawing should state the hole diameter, the pitch and pattern (straight or staggered), the open area percentage, the margin width, the gauge, the alloy and temper, the coating system and its standard, and the flatness tolerance. Leaving any of these to the fabricator invites a substitution that changes the visual result or the structural behavior.
The flatness tolerance deserves special attention. A solid panel might be specified to a 0.5% flatness limit, but a large perforated panel will rarely hit that without heavy stiffening. Setting a realistic flatness target, tied to the support spacing and the gauge, is better than copying a solid-panel tolerance and then fighting about it on site. Standards such as ASTM B209 for aluminum sheet and the relevant flatness tables give both parties a neutral reference.
For the coating, the specification should name the standard rather than a vague "PVDF" label. AAMA 2605 is the accepted benchmark for architectural PVDF, and a ISO-based quality system at the coating line is a reasonable expectation. The specifier should also state whether the panel is punched before or after coating, because that decision changes the corrosion story at the hole edge.
Engineering Advice for the Next Perforated Facade
The round hole aluminum perforated sheet earns its place on a facade because it is the most controllable way to deliver transparency, ventilation, and shading in a durable metal skin. The control comes at a price: open area drives gauge, gauge drives flatness, and the punched edge drives the entire corrosion strategy. A specification that fixes the hole pattern, the alloy, the coating sequence, and the support spacing before pricing will produce a panel that performs as drawn. A specification that treats the perforation as a decorative afterthought will produce a panel that oil-cans, corrodes at the edges, or costs far more than the bid suggested.
The practical sequence for any project is to lock the visual pattern first, run the wind and deflection checks on the chosen gauge, confirm the coating process against the environment, and only then release the support frame for pricing. Suppliers with genuine perforated-cladding experience, such as Futeng®, can provide the gauge and flatness guidance that turns an architectural pattern into a buildable panel, but the final engineering responsibility always rests with the facade engineer who signs the drawing.