Engineering Wind Load Flatness and Coating for a Perforated Sheet Facade in Solid Aluminium
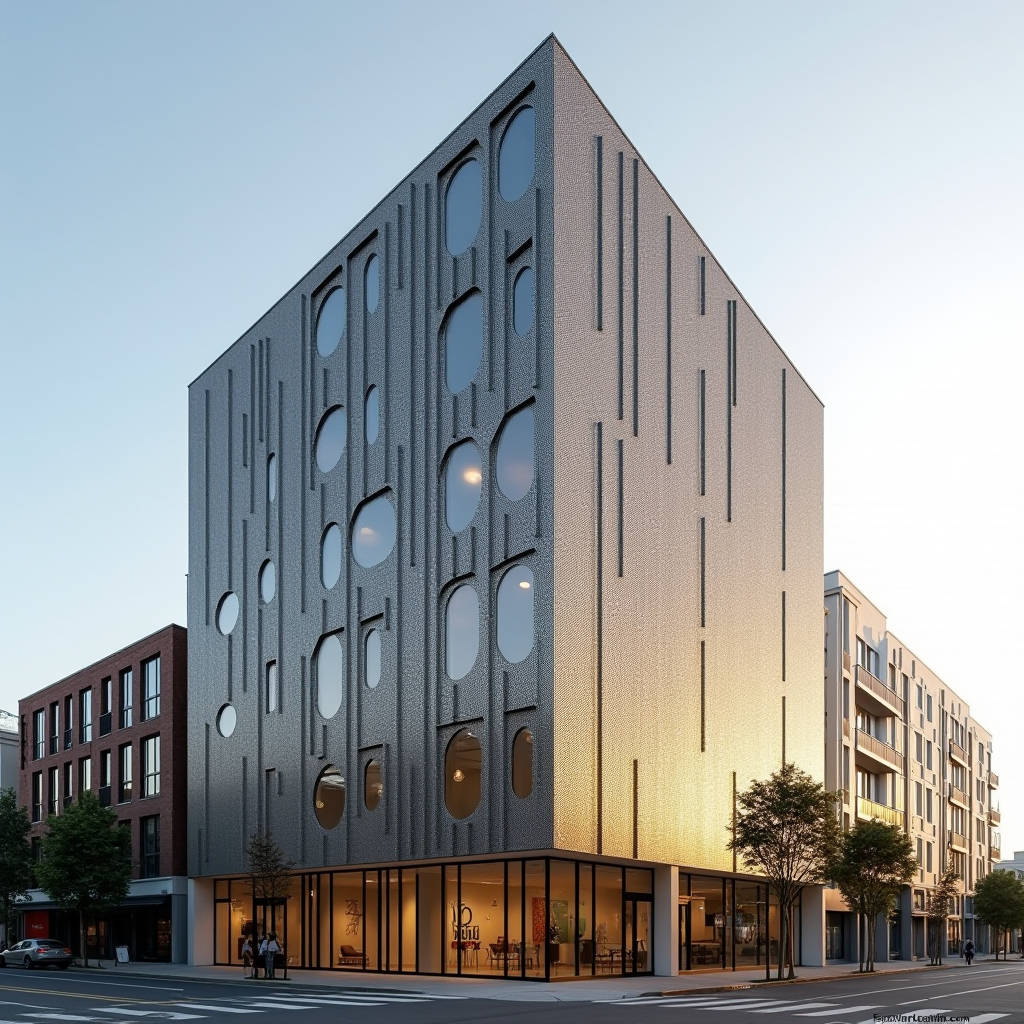
A perforated sheet facade does more than dress a building. When a solid aluminium panel is punched with a controlled pattern of holes, it becomes an engineered layer that manages daylight, ventilation, wind pressure, and solar gain at the same time. For main contractors and facade installers, the real challenge sits not in the visual idea but in the numbers behind it: open area ratio, panel deflection under wind load, and how the punching pattern changes the structural behaviour of a 2.5 mm or 3.0 mm solid aluminium sheet. This article works through the load path of a perforated panel, the thickness and ribbing decisions that keep it flat, and the fabrication tolerances that separate a facade that reads crisp from one that waves across the elevation. It is written for teams that need to specify, price, and install perforated sheet facade systems without inheriting a warranty problem later.
What Changes When You Punch Holes in a Solid Aluminium Sheet
A solid aluminium cladding panel resists wind load as a continuous plate. The moment you introduce perforations, you remove material from the very zones that carry bending stress, and you create hundreds of small stress concentrations at the hole edges. Two parameters drive the engineering conversation: the open area ratio and the hole geometry.
Open area ratio is the percentage of the panel surface that is void. A facade with 15% open area behaves almost like a solid panel; a facade with 40% open area behaves like a mesh. Most architectural perforated sheet facade work lands between 20% and 35%. Hole shape matters just as much. Round holes distribute stress evenly around the circumference and are the least expensive to punch. Square and slot perforations create sharp corners that concentrate stress, which can force a thicker base sheet or closer stiffener spacing to keep deflection within limits.
The perforation process itself also changes the material. Punching cold-works the metal around each hole and leaves a slight burr on the exit side. A well-run fabrication shop deburrs and flattens the sheet after punching, then applies the PVDF coating system over the finished perforated surface. If the coating is applied before punching, every hole edge is left as bare aluminium, which becomes a corrosion and appearance failure point within the first years of service.
Reading Wind Load on a Perforated Sheet Facade
Wind pressure does not disappear because the panel has holes in it. A perforated panel still carries a significant share of the design wind load, and the holes generate local turbulence that can cause vibration and fatigue if the panel is undersized. The governing calculation starts with the project wind zone, then applies a pressure coefficient that accounts for the open area.
For a quick estimate, a facade with 30% open area in a 1.5 kPa design wind zone can be treated as carrying roughly 70% of the full solid-panel load, though the exact figure depends on hole size and spacing. A 2.5 mm solid aluminium sheet with 25% round-hole perforation and 600 mm stiffener spacing will typically hold a 3.0 m span flat under that load. Drop the base sheet to 2.0 mm at the same open area and span, and mid-panel deflection can exceed the L/90 limit that most facade specifications reference.
The practical answer for most projects is a combination of three levers: base sheet thickness, stiffener layout, and panel size. A 3.0 mm sheet allows larger panels and wider stiffener spacing, which reduces the number of visible fixings and speeds up installation. A 2.0 mm sheet lowers material cost but demands a denser subframe, so the total installed cost often ends up higher than the thicker sheet once labour and secondary framing are counted.
Thickness, Stiffeners, and the Flatness Problem
Flatness is where perforated sheet facade projects succeed or fail visually. A solid panel can hide minor waviness behind its continuous surface. A perforated panel cannot, because the eye reads the grid of holes and any deviation in the plane becomes immediately obvious, especially in low-angle morning or evening light.
Three decisions control flatness. First, base sheet thickness: 2.5 mm and 3.0 mm solid aluminium sheets hold their plane far better than 2.0 mm after punching. Second, stiffener design: folded aluminium stiffeners or hat sections bonded to the rear face, sized and spaced so that the panel does not oil-can between supports. Third, the punching sequence: the sheet must be flattened after perforation and before coating, because punching releases internal stress and causes the sheet to bow.
A common specification gap is failing to state a flatness tolerance for the perforated panel. Solid panel specs often allow a 0.5% deviation of the diagonal dimension. For a large perforated sheet facade panel, a tighter tolerance of 0.3% or better is achievable and worth writing into the contract. Futeng® has supplied perforated solid aluminium panels to projects where the flatness tolerance was the deciding factor in the facade award, precisely because the punching and flattening process was controlled in-house rather than outsourced.
Coating Systems and the Edge Corrosion Risk
Every hole in a perforated sheet facade creates an exposed edge. The coating system must therefore be applied after perforation, and it must wrap into each hole to protect the cut edge. PVDF fluoropolymer coatings are the standard for exterior solid aluminium cladding, and the specification should state the film thickness clearly.
For a perforated panel, a three-coat PVDF system with a total dry film thickness of 30 to 40 microns is the baseline. The primer layer provides adhesion and corrosion resistance, the colour coat carries the finish, and the clear topcoat adds gloss control and UV protection. On a perforated panel, the coating must be applied so that it reaches into the hole interior, which requires a controlled line speed and spray angle rather than a simple flat-sheet pass.
The table below compares the performance characteristics of the coating options most relevant to a perforated sheet facade, so that specifiers can weigh cost against service life.
| Coating System | Typical Dry Film Thickness | Edge Coverage on Perforations | Colour / Gloss Retention | Relative Installed Cost |
|---|---|---|---|---|
| Two-coat PVDF | 25 – 30 microns | Adequate, thinner on hole edges | Good, 15 – 20 year range | Low |
| Three-coat PVDF | 30 – 40 microns | Good, full wrap into holes | Excellent, 20 – 25 year range | Moderate |
| Four-coat PVDF (primer + barrier + colour + clear) | 40 – 50 microns | Excellent, full edge encapsulation | Excellent, 25+ year range | High |
| PVDF with anti-corrosion edge sealant | 30 – 40 microns plus sealant | Superior in coastal zones | Excellent in marine environments | Highest |
The choice should follow the project environment. A perforated sheet facade in an inland city can perform well with a three-coat PVDF system. A coastal or industrial site, where chloride or sulphur compounds attack exposed edges, justifies the four-coat system or an edge sealant, because the hole edges are the first place corrosion will appear.
Fabrication Tolerances That Show Up on the Elevation
A perforated sheet facade is unforgiving of sloppy fabrication. Because the hole pattern repeats across the elevation, any variation in hole position, pitch, or panel size becomes a visible seam. The tolerance chain starts at the punch tool and ends at the installed panel joint.
The critical tolerances to write into a perforated sheet facade specification are:
- Hole diameter tolerance: plus or minus 0.1 mm on the punched hole, so the pattern reads uniform.
- Hole pitch tolerance: plus or minus 0.2 mm between hole centres, to prevent pattern drift across a panel.
- Panel length and width: plus or minus 1.0 mm for panels up to 3.0 m, so that joints stay parallel.
- Panel squareness: a diagonal difference of 2.0 mm maximum, otherwise the panel racks and the joint opens.
- Flatness after perforation: 0.3% of the diagonal dimension or better, measured before coating.
These numbers are not aspirational. They are the difference between a facade that looks continuous and one where every panel boundary catches the light differently. When the punch tooling is worn, the hole edges become ragged and the burr height increases, which shows up as a dull, grey line along each hole under direct sun.
Structural Fixing and the Subframe Load Path
A perforated sheet facade panel is fixed to its subframe differently from a solid panel in one important respect: the fixings cannot always land on solid material. With a high open area ratio, the fixing points must be positioned in the unperforated margin zones or on the rear stiffeners, not through the hole field.
The standard approach is to leave a solid perimeter margin of 30 to 50 mm around each panel, where no holes are punched. This margin carries the fixing loads and provides a clean visual frame. For larger panels, intermediate stiffeners are bonded or welded to the rear face, and the panel is fixed through those stiffeners so that the perforated field itself carries no concentrated load.
The subframe behind a perforated sheet facade also does more work than behind a solid facade. Because the panel is lighter per square metre, wind suction can lift it more easily, so the fixing design must account for both positive and negative pressure. A mechanically fixed system with aluminium angles or a cassette system with a positive locking return is preferred over adhesive-only fixing, which offers no redundancy on a perforated panel.
Cost Drivers and a Realistic Budget Estimate
Pricing a perforated sheet facade by the square metre of finished elevation is misleading, because the open area ratio changes the material, the punching time, and the coating effort. A useful way to structure the estimate is to separate the material, fabrication, coating, and installation components.
As a planning figure, a 2.5 mm solid aluminium perforated panel with 25% open area, three-coat PVDF, and a standard stiffener layout typically lands in the range of USD 90 to 140 per square metre of panel surface ex-works, depending on hole pattern complexity and coating colour. A 3.0 mm panel at the same open area adds roughly 12% to 18% to the material cost but can reduce subframe and labour cost enough to offset the difference on a large elevation.
The hole pattern itself is a hidden cost driver. A simple staggered round-hole pattern with a single diameter is the least expensive. Mixed hole sizes, slot patterns, or a custom graphic punched into the panel require tool changes and slower line speeds, which can add 20% to 40% to the fabrication cost. Specifying one hole diameter and one pitch across the entire elevation is the single most effective way to control the budget of a perforated sheet facade.
Specifying a Perforated Sheet Facade That Lasts
The decisions that determine whether a perforated sheet facade performs are made in the specification, not on site. The load path, the coating sequence, and the tolerance chain must all be written down before the first sheet is punched.
A robust specification for a perforated sheet facade should state the base sheet alloy and temper, the exact open area ratio and hole geometry, the post-perforation coating sequence with dry film thickness, the stiffener design and fixing method, and the flatness and dimensional tolerances. Reference standards such as AAMA 2605 for high-performance PVDF coatings, ASTM B209 for aluminium sheet specification, and ISO 9227 for salt spray corrosion testing give the specifier a defensible technical basis.
The most common failure pattern on a perforated sheet facade is not a dramatic collapse. It is a slow accumulation of small problems: hole-edge corrosion where the coating was applied before punching, panel waviness where the sheet was not flattened after perforation, and pattern drift where the punch tooling was worn. Each of these is preventable at the specification and fabrication stage, and each is far more expensive to correct after the panels are on the wall.
For the teams that buy and build these facades, the recommendation is consistent: fix the open area ratio early, choose the base sheet thickness from the wind load rather than from habit, apply the coating after perforation, and write the flatness and hole tolerances into the contract. A perforated sheet facade specified this way holds its plane, keeps its colour, and reads as one continuous surface for decades.